Profile Projector Wholesale Sourcing Guide for Bulk Buyers
2026-09-19
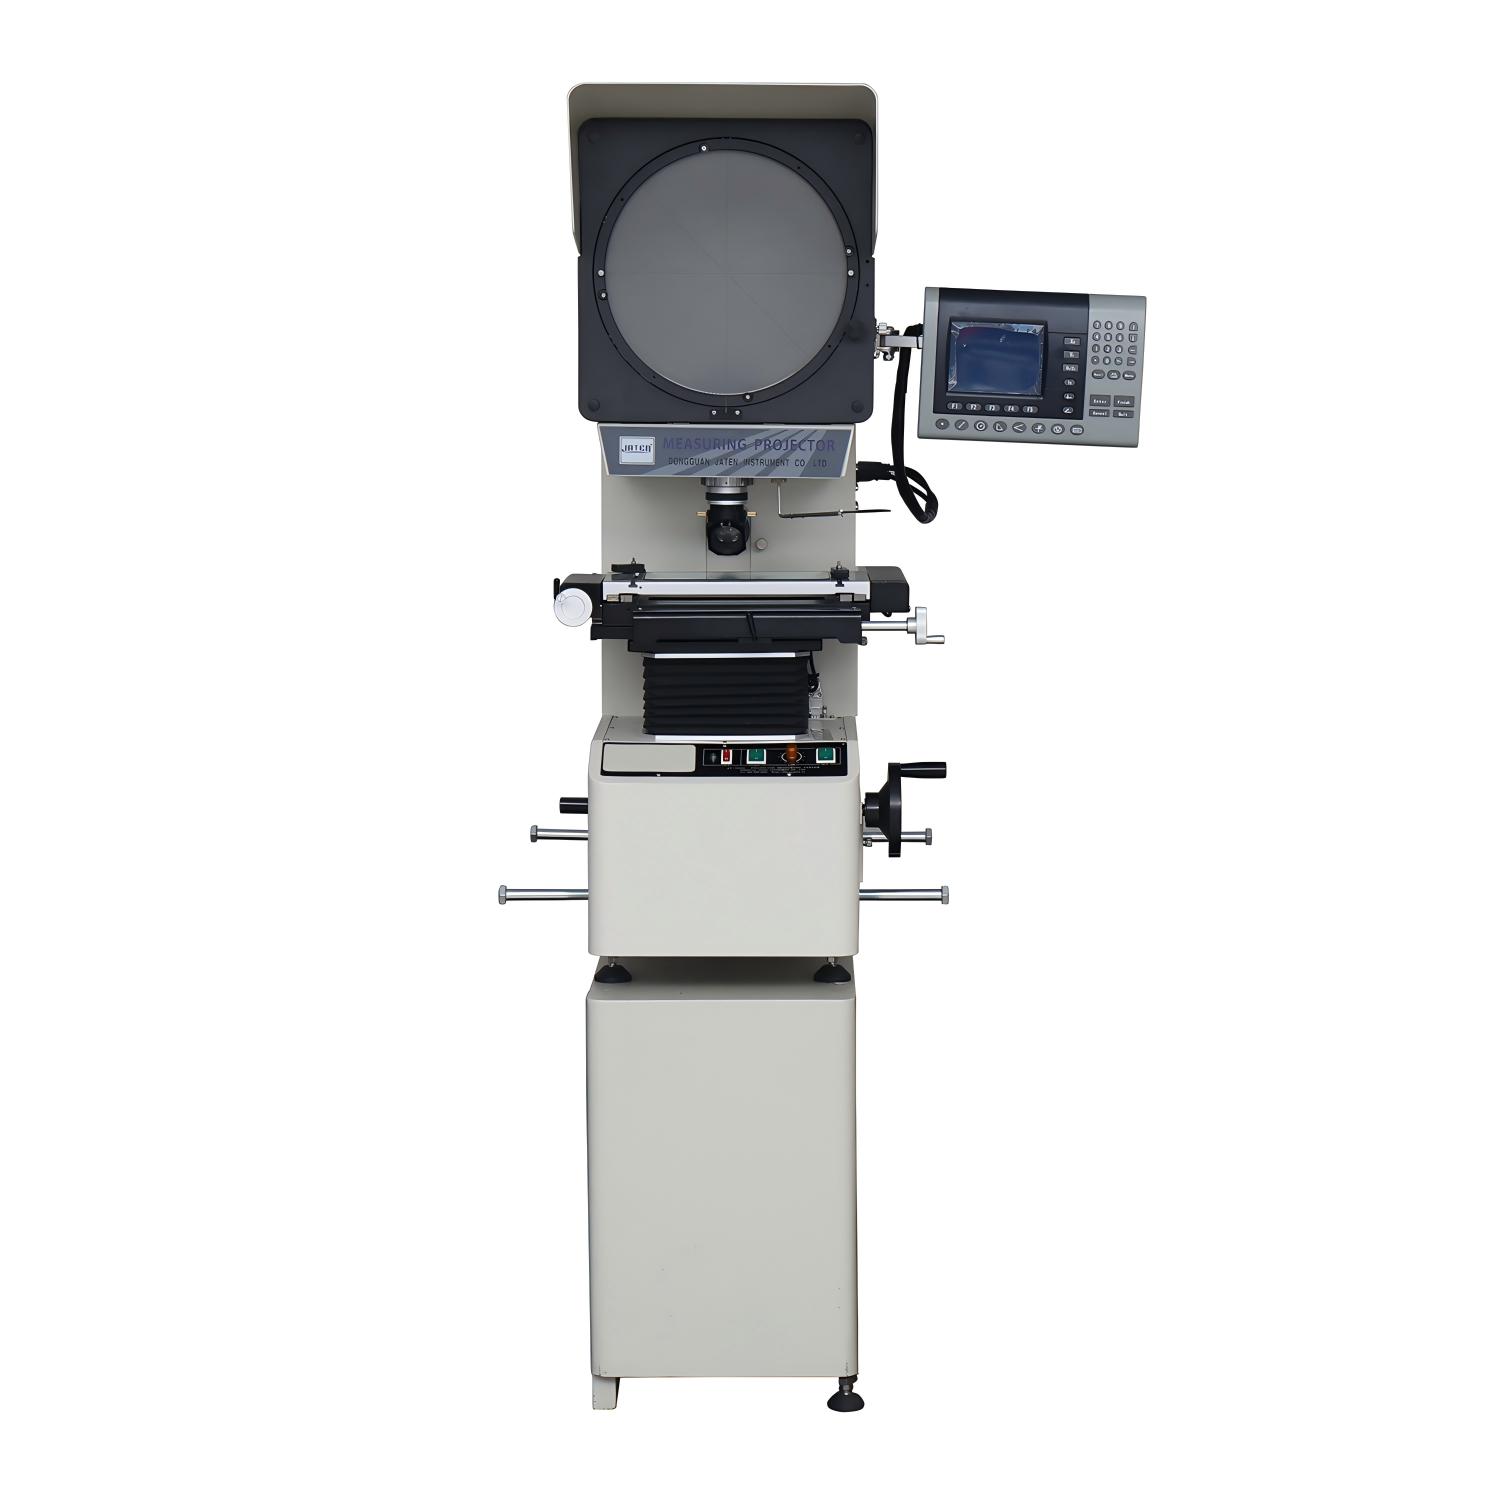
Sourcing profile projectors at wholesale prices is rarely straightforward—bulk buyers often face a minefield of vague specs, inflated quotes, and suppliers who disappear after the first shipment. This guide strips away the guesswork, giving you a practical framework to compare manufacturers, verify precision, and lock in volume pricing without sacrificing quality. If you're looking for a supplier that actually understands optical measurement and large-order logistics, JATEN has built its reputation on exactly that.
Reading a Profile Projector Quote Like a Factory Floor Veteran
A real shop quote gets a quick scan for the obvious: overall envelope, stage travel, and magnification range. But a veteran doesn't stop at headline numbers. They look for the type of illumination—profile versus surface lighting—and whether the quote bundles both, because trying to inspect a turned shoulder with only a contour light is a setup for frustration. Also watch how the stage size is described. A 12-inch screen means little if the X-Y travel can't handle your largest part without repositioning.
Next comes the fine print on accuracy and repeatability. Instead of accepting a single micron claim, compare how the spec is written: is it at the center of travel or across the full measuring range? A low price often hides a tolerance that only holds near the zero point. Veterans also check the lens options. If you're cutting threads or checking gear forms, the quote should include higher magnification lenses, not just a standard 10x. Missing accessories like a digital protractor or edge detection tell you the seller may not understand the work.
Finally, pull the quote apart for what happens after delivery. Ask about calibration intervals, service lead times, and whether software updates are included. A cheap machine with a six-week repair turnaround can idle a production cell. If the vendor won't agree to an on-site demo with your hardest part, the quoted specs are just paper. Real confidence comes from seeing the comparator handle a rechucked casting or a flimsy stamping without wobble—and that's the difference between buying a box and buying an inspection tool.
The Specs That Separate Showroom Demos from Daily Inspection Work
Showroom lighting makes every screen look bright and every housing feel solid. Pull the same device into a pre-shift walkaround on a rainy loading dock and the differences surface fast. A demo unit with a 400-nit display and glossy glass becomes a mirror the moment you step outside. Daily inspection work demands something closer to 600 nits with a matte finish, and it needs to stay readable through polarized safety glasses, not just for a quick photo op.
Battery ratings are another common bait-and-switch. A unit that idles through a two-hour trade show loop may post an eight-hour spec, but continuously cycling barcode scans, LTE uploads, and screen wake events on a cold warehouse floor can cut that figure by a third or more. Swappable batteries stop being a luxury after the second missed handoff between shifts. IP ratings get quoted on the box, yet the real test is whether the charging contacts survive repeated exposure to dust, moisture, and the occasional drop from a forklift seat—most showroom models never have to answer that.
Then there's the software. Demo modes run canned data sets that make dashboards look instant and analytics feel predictive. In the field, the spec that matters is how long a sensor or reader takes to re-acquire a signal after coming out of a dead zone, or how gracefully the interface degrades when connectivity drops mid-task. That kind of behavior never shows up in a polished walkthrough, but it decides whether a tool gets used every shift or left on the shelf after the first week.
Questions That Make Suppliers Reveal Their Real Lead Times
When you ask a supplier for lead times, the first answer is usually optimistic. The real trick is to dig into the specifics. Instead of accepting "about four weeks," ask what happens in week one versus week three. Which components have the longest procurement chain? What does their internal queue look like right now? Those questions force a supplier to move from a sales pitch to an operational reality.
Another angle is to ask about past failures. Not in a confrontational way, but from a planning perspective: "When was the last time you missed a deadline for a similar order, and what caused it?" Suppliers rarely expect this. The answer reveals bottlenecks—material shortages, customs delays, machine breakdowns—that never show up on a glossy timeline. If they hesitate or give a vague answer, that's your signal.
Finally, ask what would make them say no to an expedited request. "If I needed this in half the time, what would break first?" This flips the conversation. You're no longer hearing the lead time they want you to believe; you're hearing the constraints they actually live with. That's where the real number hides.
Where Bulk Profile Projector Orders Leak Money Before Shipping
The first leak often happens at the specification handoff. Buyers compress drawing tolerances across an entire projector batch, but only a handful of stations actually need the tighter range. Suppliers then quote for worst-case optics and surface plates, inflating unit cost before a single casting is machined. Even worse, changes after the purchase order—like swapping a digital readout for a vision system on just ten of sixty units—get billed as engineering revisions, not as standard line items.
Pre-shipment calibration is another quiet drain. Some factories run the full ISO 17025 procedure on every unit, then repeat it because the first certificate's serial numbers don't match the packing list. The third-party inspector's travel, the re-test hours, the overnight courier for corrected documents—these are rarely itemized. They surface as a lump "handling and documentation" charge that procurement signs off without audit.
Packaging and consolidation soak up the rest. Bulk orders get split across two or three container loadings due to last-minute schedule changes, so each partial lot pays full freight and insurance. Custom crates built for a 40-unit consignment often get discarded when a buyer trims the order to 25 after production. The scrap, the storage fees, the second set of export documents—all happen before the projectors leave the dock. That money is gone, and no invoice flags it as avoidable.
Building Your Own Acceptance Test for Container-Load Deliveries
A solid acceptance test starts with a clear picture of what “good” looks like when the container doors swing open. You are not just counting boxes; you are verifying that the load matches the packing list, the pallets are stable, and nothing shifted during transit. Begin by listing the non-negotiable checks: seal integrity, item counts per SKU, visible damage, and correct labeling. Write these down as a simple checklist that a warehouse associate can follow without second-guessing. The goal is to catch problems before the goods enter your inventory, not after they have disappeared into a rack.
Once the basics are covered, decide how much sampling makes sense for your operation. For high-value or fragile items, a full count might be worth the extra unloading time. For bulk, uniform cartons, a random sample of a few pallets per container often exposes systemic issues without grinding receiving to a halt. Pair the physical checks with a quick document review: compare the bill of lading, commercial invoice, and your purchase order line by line. Even a minor mismatch here can signal a bigger discrepancy in the actual cargo.
Finally, make the test repeatable and tied to real consequences. If a container fails, what happens next? Flag the load for quarantine, notify the supplier with photos, and record the variance in a shared log. Over time, these records become your best tool for spotting patterns, such as recurring damage from a particular carrier or consistent miscounts from one vendor. A well-built acceptance test is not a one-time exercise; it is a living procedure that quietly protects your inventory accuracy and your bottom line.
Keeping Wholesale Suppliers Accountable After the First Invoice
The first invoice often sets the tone for the entire supplier relationship, but it rarely reveals the full picture. Once initial payment clears, some wholesalers quietly relax their standards, shipping later, swapping materials, or ignoring agreed-upon quality checks. To keep them accountable, build a simple post-invoice review rhythm: compare actual delivery times against the quote, inspect a random sample from each new batch, and flag any discrepancy in writing within 48 hours. Small lapses that go unchallenged tend to become permanent habits.
One effective lever is tying future order volume to demonstrated consistency, not just price. A supplier who knows that repeat business depends on meeting the exact specs you set after that first invoice will self-correct before problems escalate. Ask for a corrective action plan whenever a shipment falls short, and keep it on file. Document every late arrival or off-spec item with photos and timestamps, then reference that history during renegotiations. Accountability works best when it is concrete, measurable, and tied to consequences the supplier actually cares about.
Finally, do not let personal rapport override performance data. A friendly sales rep can make you overlook a pattern of small failures until they become costly. Instead, schedule a brief monthly check-in where both sides review the same scorecard: fill rate, lead time accuracy, defect rate, and responsiveness. This turns accountability into a shared routine rather than an occasional confrontation. When suppliers know you are watching the details after the first invoice, they are far more likely to keep their promises on the tenth invoice and beyond.
FAQ
Focus on measuring range, magnification accuracy, and stage travel rather than just screen size. A machine with a slightly smaller screen but better optics and a sturdier stage often outperforms a larger display with mediocre resolution. Also ask about the linear encoder resolution and whether the manufacturer provides calibration certificates with each unit.
Ask for references from buyers who have ordered similar volumes in your region, not just brochures. Request a video walkthrough of their production floor or a live call showing the assembly area. Check whether they handle their own casting and machining or outsource critical parts, because in-house control usually means tighter tolerances and fewer hidden defects.
Beyond the unit price, factor in calibration certification, spare halogen or LED bulbs, protective covers, and freight with proper crating. Some sellers quote low machines but then charge separately for DRO boxes, lenses, or even software unlocking. Get a line-item breakdown before signing anything.
A 10x lens covers a broad range of inspection tasks, but if your clients measure fine threads or small electronic parts, add a 20x or 50x lens as an optional upgrade. Buying extra lenses together with the main order usually costs less than ordering them later, and it gives your own customers more configuration choices.
Negotiate a pre-shipment inspection clause that lets you or a third party check a random sample from the batch. Ask for the factory's own outgoing QC report and compare it with your sample measurements. If possible, request that all units be run through the same calibration fixture on the same day to reduce variation.
At minimum, ask for a two-year warranty on optical components and access to replacement bulbs and glass scales without long lead times. Find out if the supplier stocks spare parts locally or ships them from the factory. A clear response time for technical support matters more than a long list of features in the manual.
Digital readouts speed up measurements and reduce operator error, but they also add cost and can fail if overloaded. For bulk buyers serving traditional machine shops, a hybrid approach works well: offer one base model with analog micrometers and an optional DRO upgrade. This way you cover both budget-conscious and high-throughput customers.
Request a traceable calibration certificate, a conformity declaration for electrical safety, and a detailed packing list with serial numbers. If you sell into regulated industries, ask whether the factory can supply ISO 17025 certificates or at least an internal QC report with measured values for every unit. These documents make resale much smoother.
Conclusion
The real work in wholesale sourcing of profile projectors isn't comparing list prices; it's reading a quote the way a production engineer reads a blueprint. A factory-floor veteran ignores the glossy demo numbers and checks whether the quote includes glass-scale resolution, optical distortion specs, and the exact type of surface and transmitted illumination. Most showroom machines can impress for fifteen minutes, but daily inspection demands thermal stability, a rigid column, and lens coatings that won't drift after three shifts. If you want honest lead times, don't ask for final assembly dates—ask how many raw castings and controller boards are actually sitting in the supplier's stockroom. That single question reveals whether the lead time is planned or just a hopeful guess.
Bulk orders tend to leak money before the container even leaves the dock. Look for what's missing: calibration certificates, spare halogen or LED lamps, protective packaging for optical glass, and even the operation manual. Too many quotes strip these out and call them optional later. For a container-load delivery, build your own acceptance test instead of trusting the supplier's word. Pick random units, run the same thread or profile standard twenty times on each, and reject anything that fails a tight repeatability and reproducibility limit. After the first invoice, keep leverage by tying extended payment terms to field calibration support, spare-parts delivery windows, and written warranty language for optical assemblies. That's how you make wholesale suppliers stay accountable instead of disappearing after the first shipment.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/