Shredder Manufacturing Concerns You Can't Afford to Overlook
2026-11-16
Every industrial operation depends on reliable shredding equipment, yet hidden manufacturing flaws can quietly sabotage performance, safety, and your bottom line. At Shengzhong Shredder, we see too many businesses learn this the hard way—through unexpected downtime, inconsistent output, and costly repairs. Before you trust your process to just any machine, let’s uncover the critical manufacturing concerns you can’t afford to overlook.
When Cutting Costs Cuts Into Safety
A factory floor supervisor, staring at a dwindling maintenance budget, quietly decides to push the hydraulic press inspection by another month. The machine has been groaning more lately, but the production targets loom larger. Three weeks later, a line worker loses two fingers. The cost savings from deferring that inspection disappear the moment OSHA fines, litigation, and downtime pile up. This is what happens when cost-cutting carves straight into safety.
Companies often treat safety training as a soft expense, first on the chopping block when quarterly numbers need a boost. They switch to online modules that employees click through half-asleep, or reduce hands-on drills that once taught muscle memory for emergency shutdowns. The logic feels airtight—until a new hire mistakes a chemical tank’s labeling and causes a toxic release. Restocking the training department later costs far more, but the real price gets measured in human harm.
There’s a peculiar maths that executives sometimes adopt: a dollar not spent on safety looks like a dollar earned. But the equation ignores property damage, legal battles, and a reputation so bruised that contracts evaporate. In a world where a single accident can bankrupt a small firm or kneecap a multinational’s brand, trimming budgets around safety isn’t frugality—it’s borrowing from disaster at an interest rate no spreadsheet can calculate.
The Blade Problem Nobody Talks About Until It’s Too Late
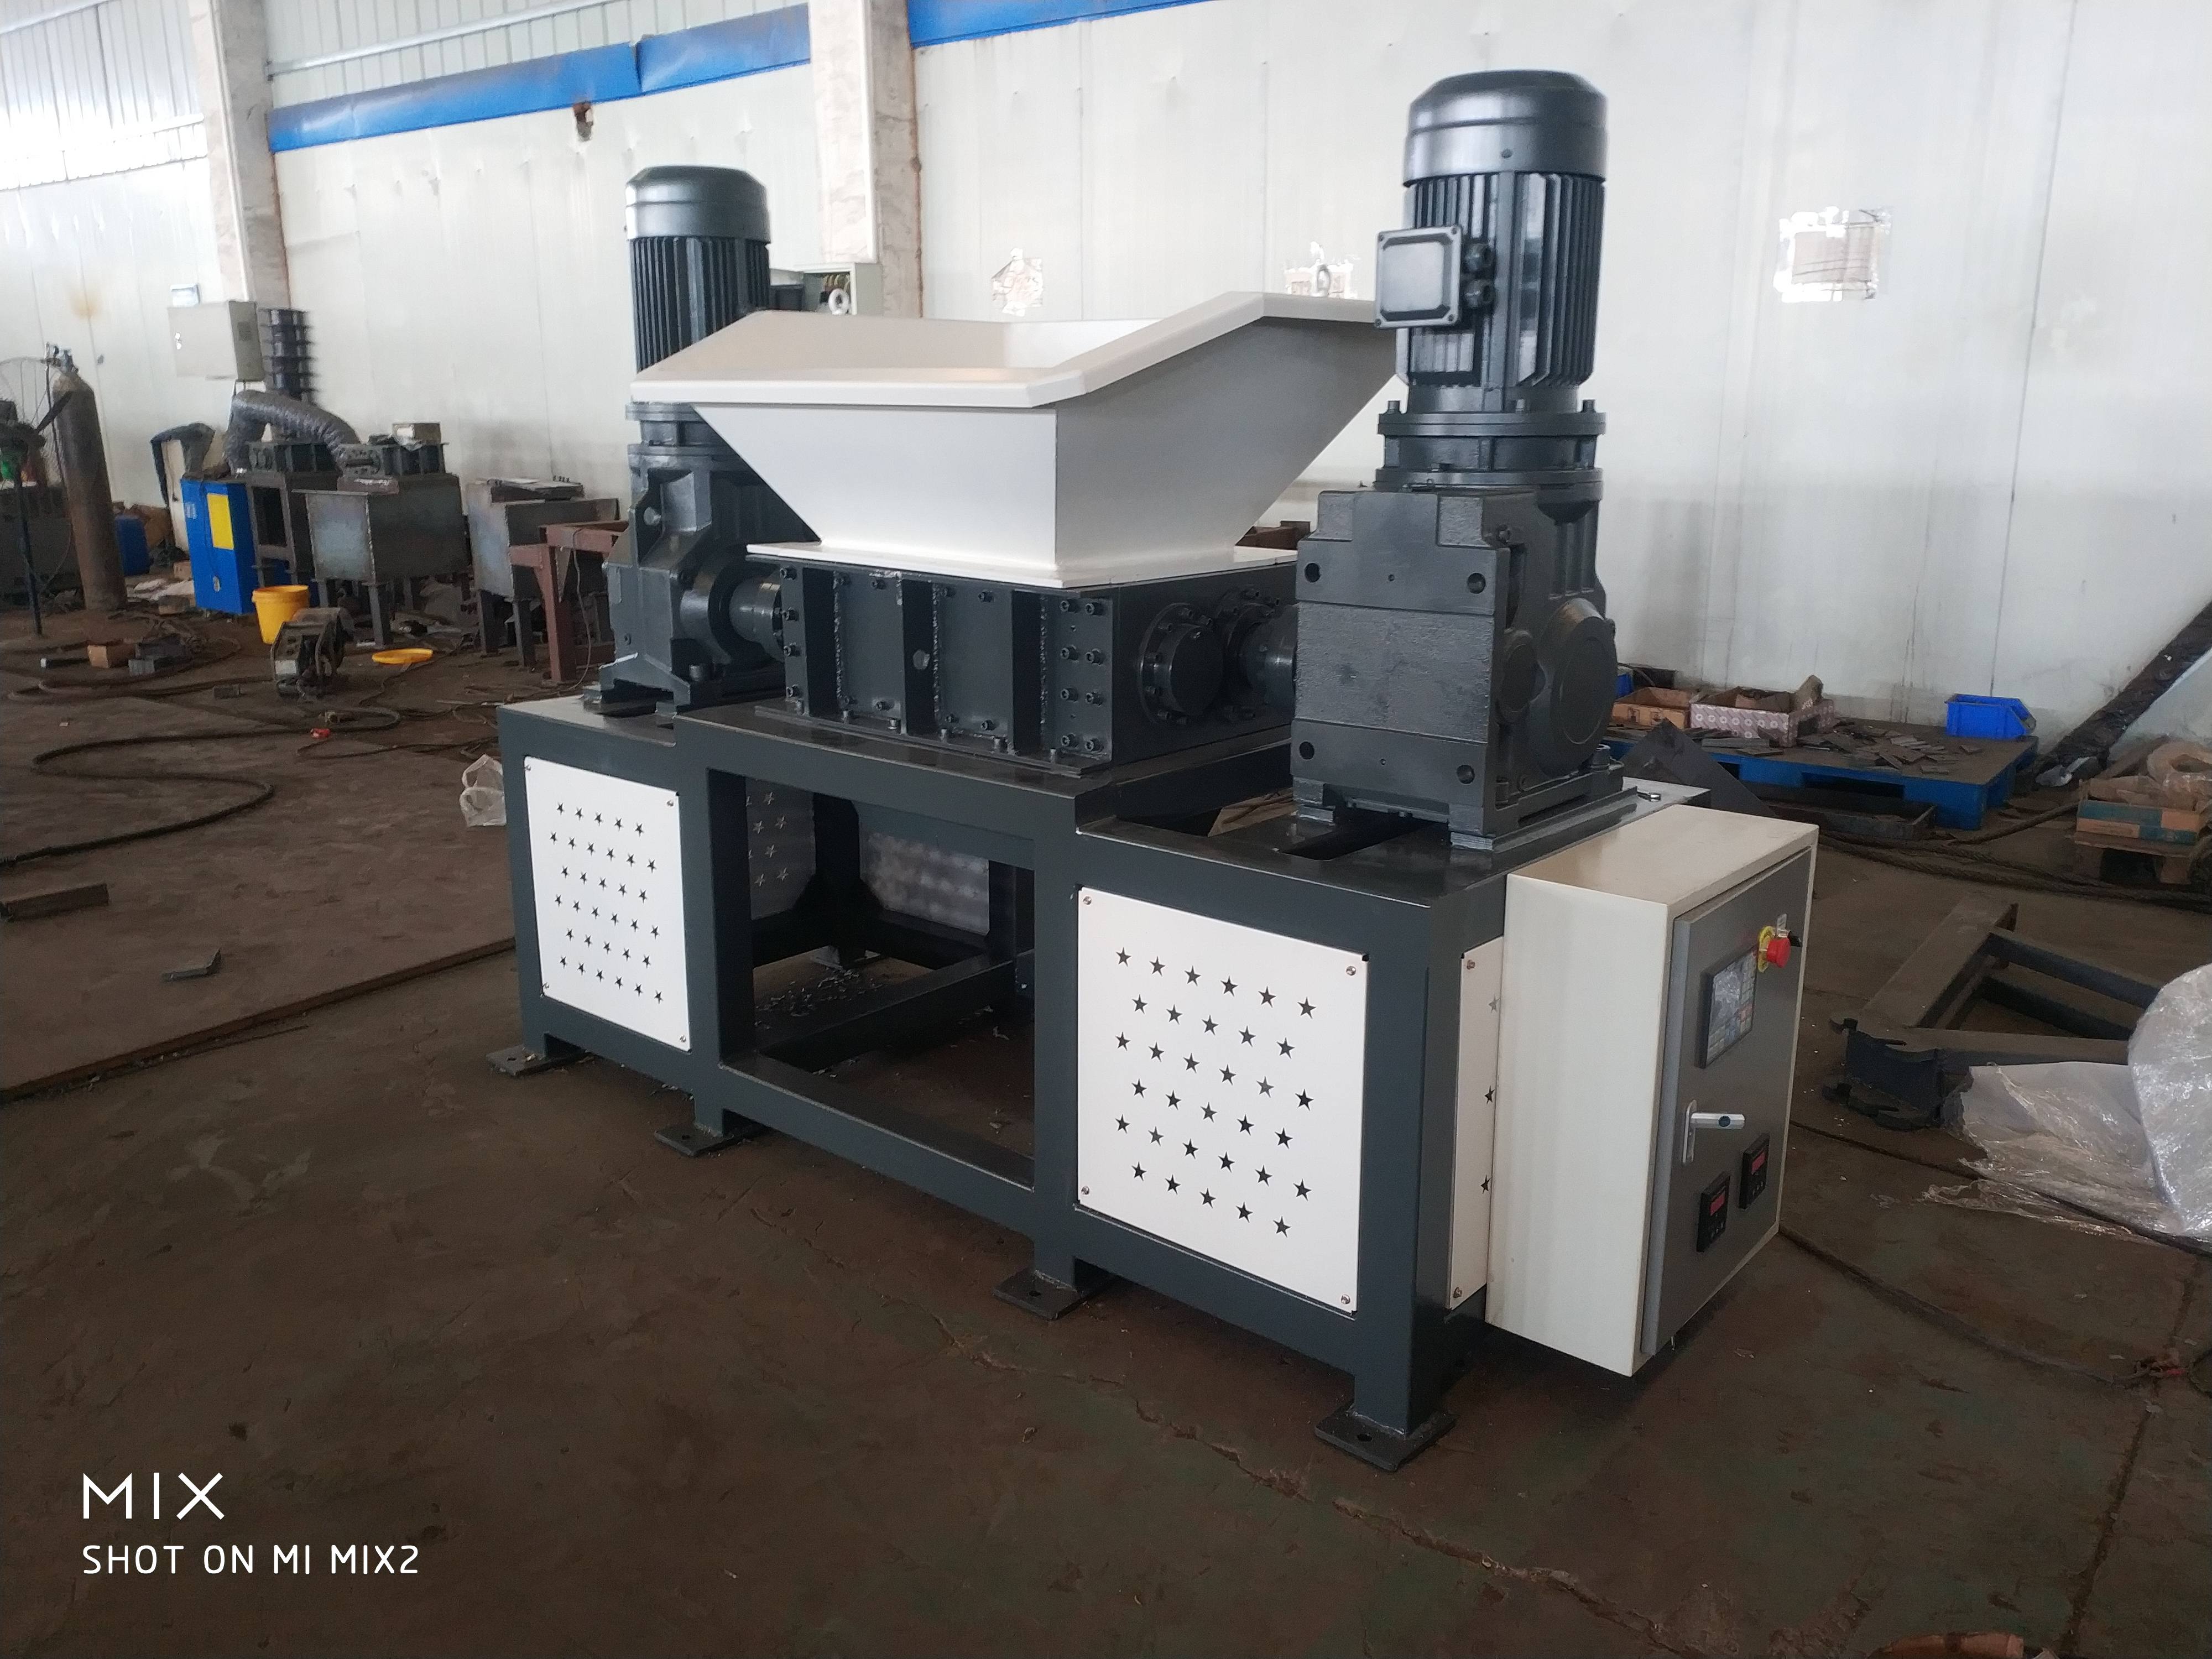
Most people only think about a blade when it’s already failing them—when the cut is ragged, the effort doubles, and the frustration sets in. But the real issue starts much earlier, in the quiet neglect of micro-imperfections that accumulate with every use. A blade doesn’t just go dull in a single moment; it loses its edge gradually, changing how you work without you even noticing. By the time you’re fighting the material instead of gliding through it, you’ve already been compensating for weeks, maybe months, with extra force and compromised precision. That’s the silent cost nobody tallies until a project is ruined or a hand slips from the added strain.
What makes this so insidious is how skill masks the decline. A seasoned hand learns to adapt—tilting the angle, applying more pressure, slowing down the pace—all while telling themselves it’s still good enough. The truth is, you’re no longer relying on the tool’s integrity but on your own muscle memory to correct its flaws. That band-aid approach works right up until it doesn’t, and often the breaking point isn’t a catastrophic failure but a creeping inconsistency that shows up in the final result. The joinery that used to fit flush now has a hairline gap. The clean bevel starts showing micro-tears. You blame technique or materials before ever suspecting the quiet culprit in your hand.
The conversation rarely happens because it’s not dramatic. There’s no loud snap, no cinematic spark—just a slow erosion that eats away at efficiency and safety. Yet ignoring it turns a trivial maintenance step into a risky gamble. Re-honing isn’t about chasing a razor edge for vanity; it’s about undoing the invisible damage before it rewrites the way you work. The blade problem nobody discusses isn’t the moment of obvious dullness, but the long, deceptive stretch where you convince yourself it still cuts just fine.
Why Your Motor Keeps Overheating — and the Real Fix
Motors rarely overheat because of a single dramatic failure. More often, it's a slow accumulation of overlooked stress—ambient dust clogging the vents, subtle voltage imbalances that force the windings to work harder than they were designed for, or a bearing that's been running a fraction too tight for months. These conditions build up heat that insulation can't shed fast enough, and the temperature creeps into a danger zone long before any alarm triggers.
The real fix isn't just adding a bigger fan or resetting the thermal overload. You have to look at what's actually driving the thermal rise. Measure the supply at the motor terminals under load, not at the panel; a 2% voltage imbalance can generate a 10°C rise you'll never see on a control-room screen. Pull the fan cover and clear out compacted debris that's acting like a blanket. And if the motor has been greased on a strict calendar schedule, stop—overgreasing pushes lubricant into the windings and bakes into an insulating crust that traps heat exactly where it shouldn't be.
Sometimes the answer is even simpler: the motor is simply the wrong tool for the job. A TEFC enclosure in a washdown area might be drowning in its own retained heat, while an open drip-proof design would breathe and run cooler. Swapping the motor for one with a proper service factor and the right enclosure class often eliminates the overheating for good, because you stop fighting a thermal problem with electrical bandaids.
Noise Levels That Signal Deeper Engineering Flaws
When a pump starts to hum a little louder than usual, it’s easy to write it off as normal wear. But shifts in sound often point to misalignment or cavitation—conditions that slowly eat away at seals and bearings. By the time the noise becomes impossible to ignore, the underlying problem has usually spread far beyond the original component, turning a simple adjustment into a multi-day tear-down.
Electrical systems offer their own version of this warning. A faint crackle near a breaker panel or a high-pitched whine from a transformer isn’t just background chatter—it hints at loose connections, partial discharges, or insulation breakdown. Ignoring these audio cues doesn’t just risk a trip; it invites progressive damage that can cascade through switchgear long before any visible sign of trouble appears.
Structural elements are no different. What starts as a rhythmic creak in a steel truss or a subtle change in the frequency of bridge stay cables can signal fatigue cracking or loss of pre-stress. Engineers who treat such sounds as diagnostic data rather than a nuisance catch flaws while they’re still confined to a single weld or tendon, avoiding failures that rewrite maintenance budgets—and sometimes safety records.
Assembly Steps Where Small Mistakes Cascade into Big Failures
A misaligned bracket on page three of the manual might seem trivial until the entire frame sits crooked, forcing downstream panels to buckle under tension. These early slips often appear cosmetic—a gap here, a slightly tilted guide—but they hijack the structural symmetry that later components depend on. By the final steps, compounding distortions demand force to fit parts that should slide together effortlessly, quietly transforming a simple build into a stress-laden puzzle.
Torque sequences bring a subtler danger. Over-tightening a single bolt ahead of its neighbors shifts load paths in ways the design never accounted for, spawning microfractures or warped sealing surfaces. The failure rarely announces itself at the torque wrench; instead, it brews silently until heat cycles and vibration exploit the uneven stress, turning a forgotten shortcut into a cracked housing or a persistent leak.
Wiring harnesses illustrate the cascade with relentless clarity. One connector pin backed out by a millimeter can pass initial checks, only to go intermittent under thermal expansion. That small flicker can confuse a control module, triggering adaptive strategies that push other systems into fault. Mechanics then chase phantom codes, replacing expensive sensors and actuators, while the real culprit remains hidden in a step most builders treat as mindless snap-together work.
Material Choices That Quietly Define a Shredder’s Reputation
Long before a shredder ever meets paper, its character is forged in the quiet selection of steel grades and alloy ratios. Most buyers glance at sheet capacity or run time, yet the real story unfolds inside the cutting head, where hardened tool steels battle fatigue cycle after cycle. Premium makers lean toward proprietary blends—D2, high-chromium variants, or boron-treated edges—that resist microchipping far longer than off-the-shelf carbon steels. It’s not just about hardness numbers on a spec sheet; it’s how those numbers translate into a throat that still bites cleanly after a decade of daily neglect.
The plastics often reveal even more. A chassis molded from glass-filled nylon instead of standard ABS tells you the manufacturer expects thermal stress, not just a quiet desk life. These choices hide in part numbers, rarely advertised, but they separate a machine that warps after a few overheating cycles from one that shrugs off a jam without cracking the main frame. Even the rubber feet carry weight—literally and figuratively—when a design chooses high-rebound silicone over generic PVC. Nobody replaces shredded gears; the initial material choice is the only warranty that ever matters.
FAQ
Hands-down, it's the unguarded nip points at feed openings and discharge conveyors. I've audited plants where operators routinely bypass interlocks to clear jams faster, not realizing a microsecond slack in concentration can cost them fingers. Another huge red flag is insufficient lockout/tagout enforcement during maintenance—someone always assumes the machine won’t restart mid-repair. And don’t forget dust collection: fine metal or plastic particles become combustible clouds that no one treats as explosive until an incident report lands on the desk.
When you spec a shaft for 4140 steel but the mill sends a batch with micro-inclusions or off-spec hardness near the keyways, fatigue cracks start whispering long before they scream. I've seen a single oversized particle from recycled plastic—contaminated with glass fillers—work-harden into a wedge and shear rotor bolts in under two weeks. Vibration monitoring won’t save you if the root cause is impurities dancing inside batch-to-batch variability that your receiving inspection never checks.
Most maintenance crews react to alarm thresholds, not the rate of change. A bearing that climbs 5°F per hour on Tuesday and 8°F per hour on Wednesday is telegraphing lube breakdown or spalling, but if the trending software only triggers at 185°F, you’re already racing toward a seizure. The real killer is moisture migration during washdown cycles—grease turns to emulsion, clearances close, and nobody notices until a shaft blues and snaps on midnight shift.
They hide inside control panels where vibration damping is an afterthought. Loose terminal strips and unsealed connectors on PLC modules develop micro-fretting corrosion that mimics intermittent sensor faults. Field guys swap sensors three times before the real culprit—a hairline fracture in a circuit board trace—kills the main drive contactor at the worst moment. Also, undersized grounding straps on trailer-mounted units create floating voltage that scrambles weighing load cells; you’ll chase phantom overload trips for weeks.
Everyone talks about hardness Rockwell numbers, but neglects retained austenite and carbide distribution in the microstructure. If the heat treater rushes the cryo step, unstable austenite transforms under impact loads mid-operation and causes micro-chipping. Plus, edge prep angles that look identical on a drawing don’t account for how the shear angle shifts when knives wear asymmetrically—once that happens, you’re no longer cutting cleanly; you’re beating the material, accelerating rollback and overheating the whole head.
Bad air pattern means classification suffers: lighter fractions recirculate along the rotor and get repeatedly hit, generating fines that clog screens and spike energy consumption. Worse, stagnant zones right below the anvil trap material that smolders from friction if you process hot feedstock. I’ve traced two hydraulic system fires back to a pocket of compacted debris that acted like a kiln because the CFD simulation was skipped at design stage. Now owners retroactively install purge air jets—expensive fix for a preventable headache.
The moment someone adjusts the spring tension to 'just get through the shift' and forgets to log the change. A clutch that slips at 120% of rated torque on a clean test bench behaves totally differently after three months of dust and humidity—the friction plates glaze, breakaway torque drifts lower, and suddenly a manageable jam becomes a full stall that twists splines or cracks the gearbox housing. Pair that with a VFD that’s set to decelerate aggressively, and you’ve installed a perfect mechanical fuse that never actually blows when needed.
It’s all about the stress risers at stiffener terminations. If a gusset plate ends abruptly perpendicular to a main longitudinal weld without a smooth radius transition, every impact pulse concentrates there like a hammer on a bell. I’ve examined cracks that propagated right along the heat-affected zone because the welding sequence wasn’t balanced to control distortion—the frame might measure square cold, but locked-in residual tension plus operational vibration equals a ticking clock that never shows up on an ultrasonic test until after painting.
Conclusion
In shredder manufacturing, the difference between a workhorse machine and a looming liability often hides in the details that quarterly reviews never capture. When cost-cutting targets override engineering integrity, blades grow brittle, housings thin out, and suddenly a machine designed to destroy material starts destroying itself—taking operator safety with it. The most insidious failures aren't sudden explosions but gradual decays: micro-cracks forming on cutting edges from substandard alloys, or motors chronically running hot because someone swapped a copper winding for aluminum to shave a few dollars. These aren't hypotheticals that surface during a quiet audit; they're the problems that announce themselves when a bin is full, a deadline is tight, and the shredder jams hard enough to send a torque spike through every compromised bearing.
What quietly defines a shredder's reputation isn't the spec sheet but the material story nobody writes down. The wrong steel grade in a blade means the difference between fifteen thousand cycles and fifteen hundred; the wrong grade of sound-dampening foam means a noise signature that masks gear misalignment until the teeth shear. Assembly matters just as much—a rushed press-fit on a shaft can propagate an eccentricity that cascades into bearing wipes, belt wear, and ultimately a motor burnout that gets misdiagnosed as “bad ventilation.” The real fix isn't chasing symptoms but acknowledging that shredders are precision systems pretending to be brute force appliances. Overlook that tension, and the market will quietly rewrite your reputation one failed unit at a time.
Contact Us
Contact Person: Leon
Email: [email protected]
Tel/WhatsApp: 8615385558866
Website: https://www.shred-waste.com